Industrial Finishing Equipment for Energy & Utility Infrastructure
PFS ZENITH SERIES
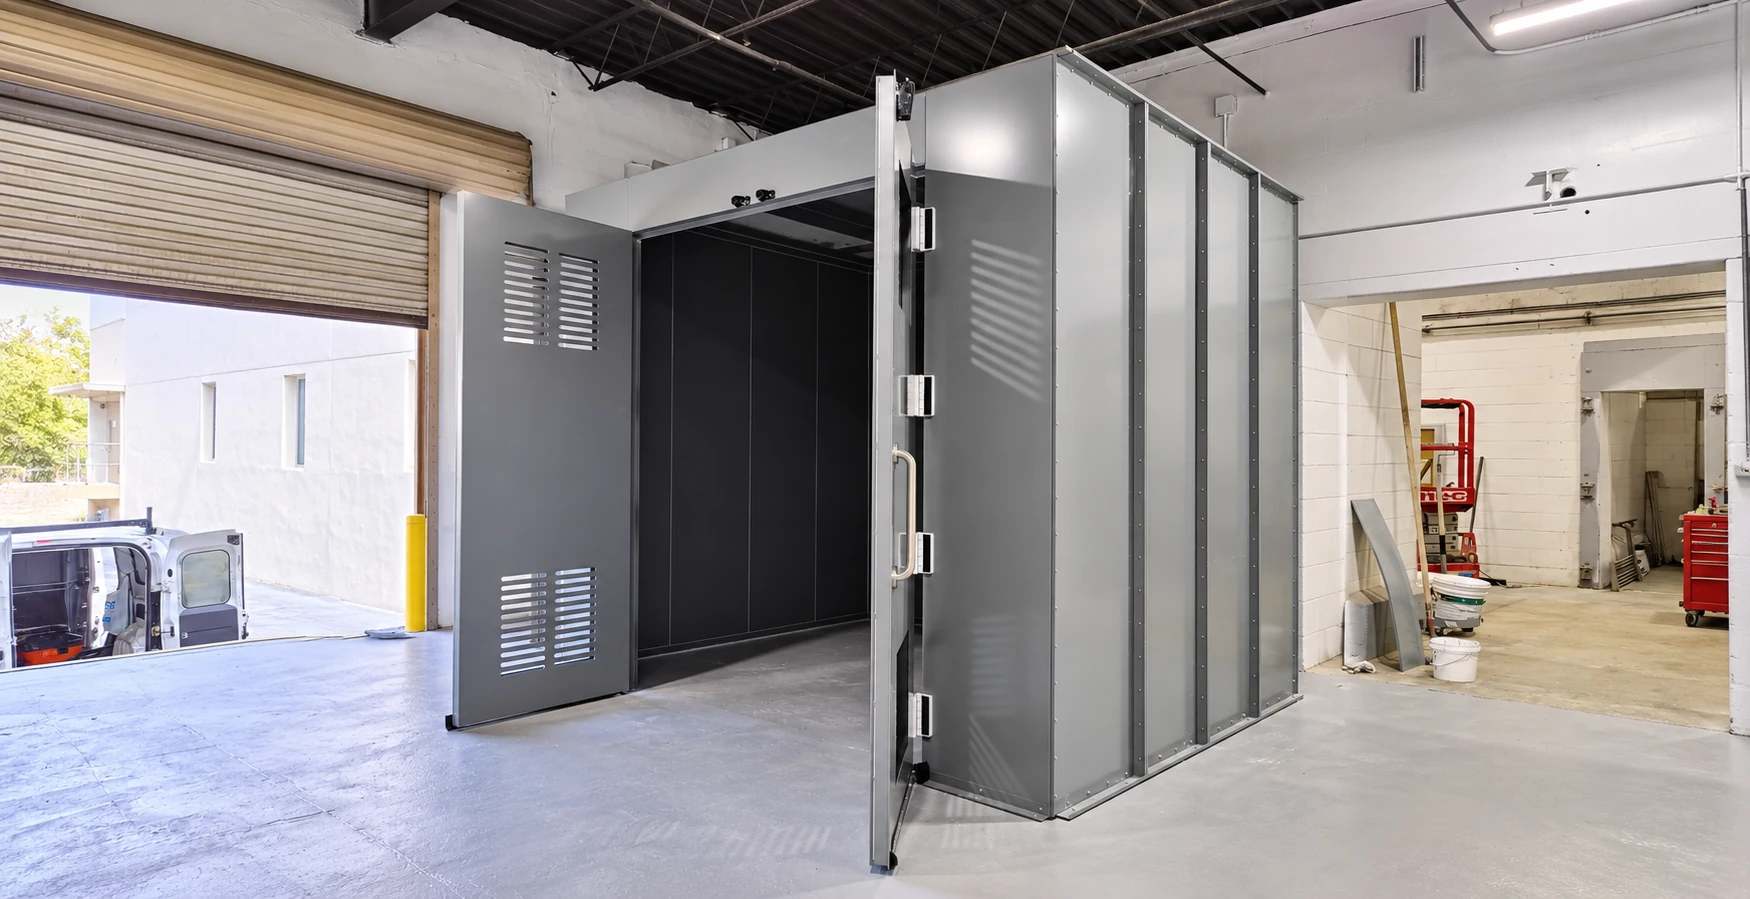
manufactured in the USA with ETL/UL listed and UL 508A certified components. Clear-span oversized construction. Engineered for transformers, switchgear, turbine components, and pipeline infrastructure — installed nationwide.
Clear-span structural steel frames engineered for transformers, switchgear cabinets, turbine components, and large pipeline sections. No interior columns. Full 360° access for large-format industrial finishing.
02
Precision Airflow for Complex Geometries
Crossflow and downdraft configurations with high-CFM fans sized for large-volume booths. Uniform air velocity across the entire work envelope — essential for consistent finish quality on complex electrical and mechanical assemblies.
03
Class I Division 2 (CID2) Lighting
Inside-access, CID2 four-tube fixtures are standard. Uniform, shadow-free illumination at 100+ foot-candles — essential for finish inspection on complex equipment surfaces, tight recesses, and precision-machined components.
04
Explosion-Safe Electrical Components
All electrical components rated for spray environments. Explosion-proof fans, CID2 lighting, and UL 508A control panels ensure compliance with NFPA 33 and OSHA standards for solvent-based coating applications.
05
PFS Core Control Panel — UL 508A
UL 508A certified control panels with spray, flash, and cure modes. Programmable cycle timers, temperature monitoring, and safety interlocks. Custom integration available for production line and utility facility environments.
NFPA 33 sets the fire-safety rules for spray areas: construction, ventilation, electrical classification, fire protection and housekeeping.
OSHA 29 CFR 1910.107 covers spray finishing in the workplace, including exhaust and filter maintenance.
The International Fire Code (or your state version, such as the California Fire Code) and the local fire marshal govern the permit and inspection.
Your local air district may require a permit to operate, VOC limits and record keeping.
EPA 40 CFR Part 63, Subpart HHHHHH (6H) applies to shops that spray coatings containing target metal HAPs (chromium, lead, manganese, nickel, cadmium). It requires an enclosed booth, filters rated at least 98% capture, HVLP or equivalent guns, painter training and notifications.
PFS booths ship with ETL-listed electrical packages, and we provide the drawings and data your permit packet needs. Requirements vary by jurisdiction, so confirm with your authority having jurisdiction. See our NFPA 33 guide.
Protective coatings
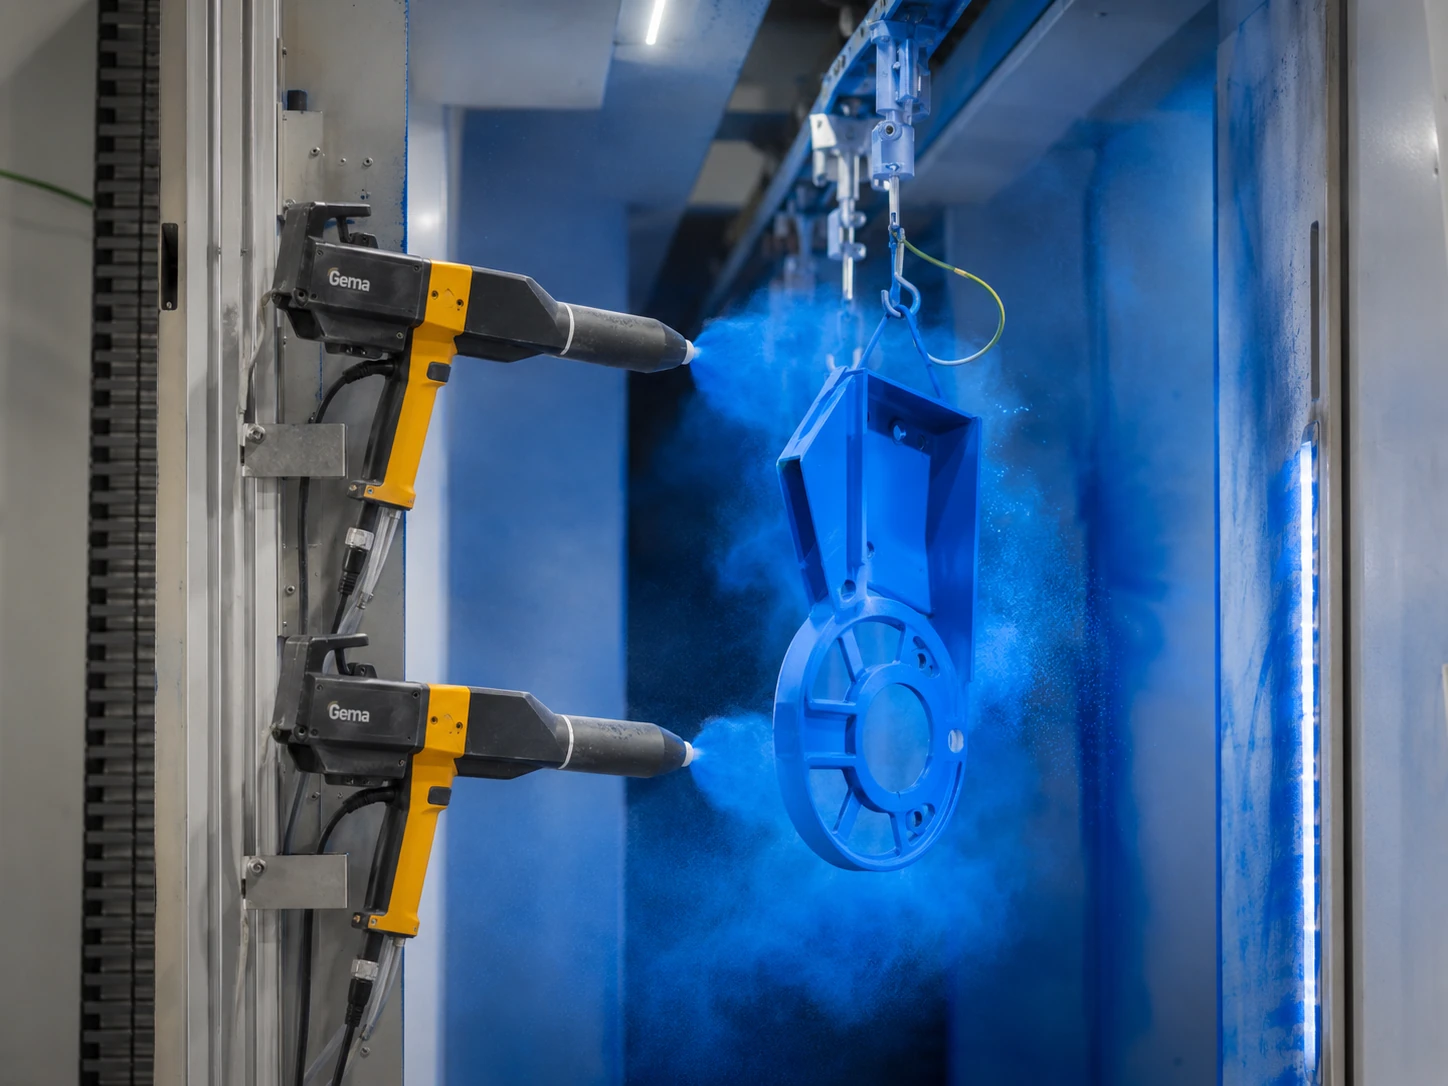
High-solids epoxies and urethanes often need controlled temperature for application and cure. A heated booth or a separate oven keeps cure times predictable through the year.
ENERGY & UTILITY GUIDE
Finishing Equipment for Energy and Utility Work
Booths, blasting and cure for energy equipment.
What gets painted
Energy and utility manufacturers and service shops coat transformers, switchgear, control enclosures, generator sets, pipe spools, tanks, towers and wind and solar components. Most of these are large, heavy and painted with high-performance industrial coatings.
Booth type and airflow
cross-flow and semi-downdraft booths handle large enclosures and assemblies economically. full downdraft gives the cleanest finish for visible equipment. open-face booths work well for smaller parts and sub-assemblies.
Surface prep and cure
Corrosion-resistant systems depend on surface prep. PFS supplies blasting systems for blast profiles and heated booths and cure ovens for multi-coat epoxy and urethane systems.
Codes and listings
Every PFS booth is built with ETL/UL listed components and engineered to NFPA 33, the NEC (Article 516) and OSHA 1910.107. Your local fire marshal and air district have the final say, so we supply drawings, airflow data and cut sheets for permitting. See our NFPA 33 compliance guide for the details.
What to send for a quote
To quote quickly, send us: the largest part (L × W × H and weight); the door opening you need; your building footprint, ceiling height and power; the coatings you spray; and how many units per day or week you finish. Photos of the space help.
Tell us your equipment dimensions.
We'll spec the booth.
Quote in 24 hours. manufactured in the USA with ETL/UL listed components. Installed nationwide by PFS-certified technicians.