
Laminar downdraft airflow. Robotic arm integration ready. Drive-through and conveyor-integrated configurations. ETL/UL listed and UL 508A certified components. NFPA 33 compliant. Engineered for OEM, Tier 1, and high-volume automotive finishing — installed nationwide.


Full downdraft airflow, bake-and-cure capability and drive-through access, built to your vehicle dimensions and production throughput.
Tap any photo to open it full size.


PFS booths ship with ETL-listed electrical packages, and we provide the drawings and data your permit packet needs. Requirements vary by jurisdiction, so confirm with your authority having jurisdiction. See our NFPA 33 guide.
PFS engineers the booth, oven, conveyor interface and controls as one system so airflow, temperatures and line speed are balanced together. See Integration & automation.
Automotive plants use spray booths for primer, base and clear on bodies and panels, for repair and spot-repair loops at end of line, for low-volume and specialty vehicles, and for components such as bumpers, trim and chassis parts. Many plants also need prep stations, mixing rooms and cure ovens around the booth.
For class-A finishes, full downdraft airflow carries overspray straight to the floor and away from the vehicle. semi-downdraft booths cost less to install because they need no pit, and they suit components and fleet work. cross-flow works for parts and fixtures where finish demands are lower.
Line rate drives booth length, the number of booths and whether you need a separate flash or bake zone. heated booths or dedicated cure ovens shorten cycle times. We size the air make-up to keep booth pressure stable through every mode.
PFS can lay out booths around existing conveyors, carts or track systems and leave openings, controls interlocks and platforms for robots or reciprocators. Tell us your carrier size and pitch early so the openings and airflow are designed around them.
Every PFS booth is built with ETL/UL listed components and engineered to NFPA 33, the NEC (Article 516) and OSHA 1910.107. Your local fire marshal and air district have the final say, so we supply drawings, airflow data and cut sheets for permitting. See our NFPA 33 compliance guide for the details.
For a quote, send: vehicle or part dimensions (L × W × H); how it moves through the plant; required door opening; building footprint, ceiling height and power; coatings; units per day or week; and photos of the space.


Yes. We engineer the booth, oven, air make-up and controls together so the system is balanced as one line.
NFPA 33, OSHA 1910.107, the local fire code and the plant air permit are the usual starting point. Requirements vary by site.
PFS builds four automotive paint booth styles: Zenith full downdraft, Helios side downdraft with no pit, Orion cross-flow and the Orion-R robotic cell. Custom drive-through, tandem and multi-zone booths are engineered to your line layout.
Yes. Integrated gas or electric heat brings PFS automotive spray booths to 140°F–180°F for faster cure cycles. Separate cure ovens can be added for line production.
PFS drive-through automotive booths come in custom widths from 12 ft to 40+ ft, for full-size vehicles and body-in-white assemblies.
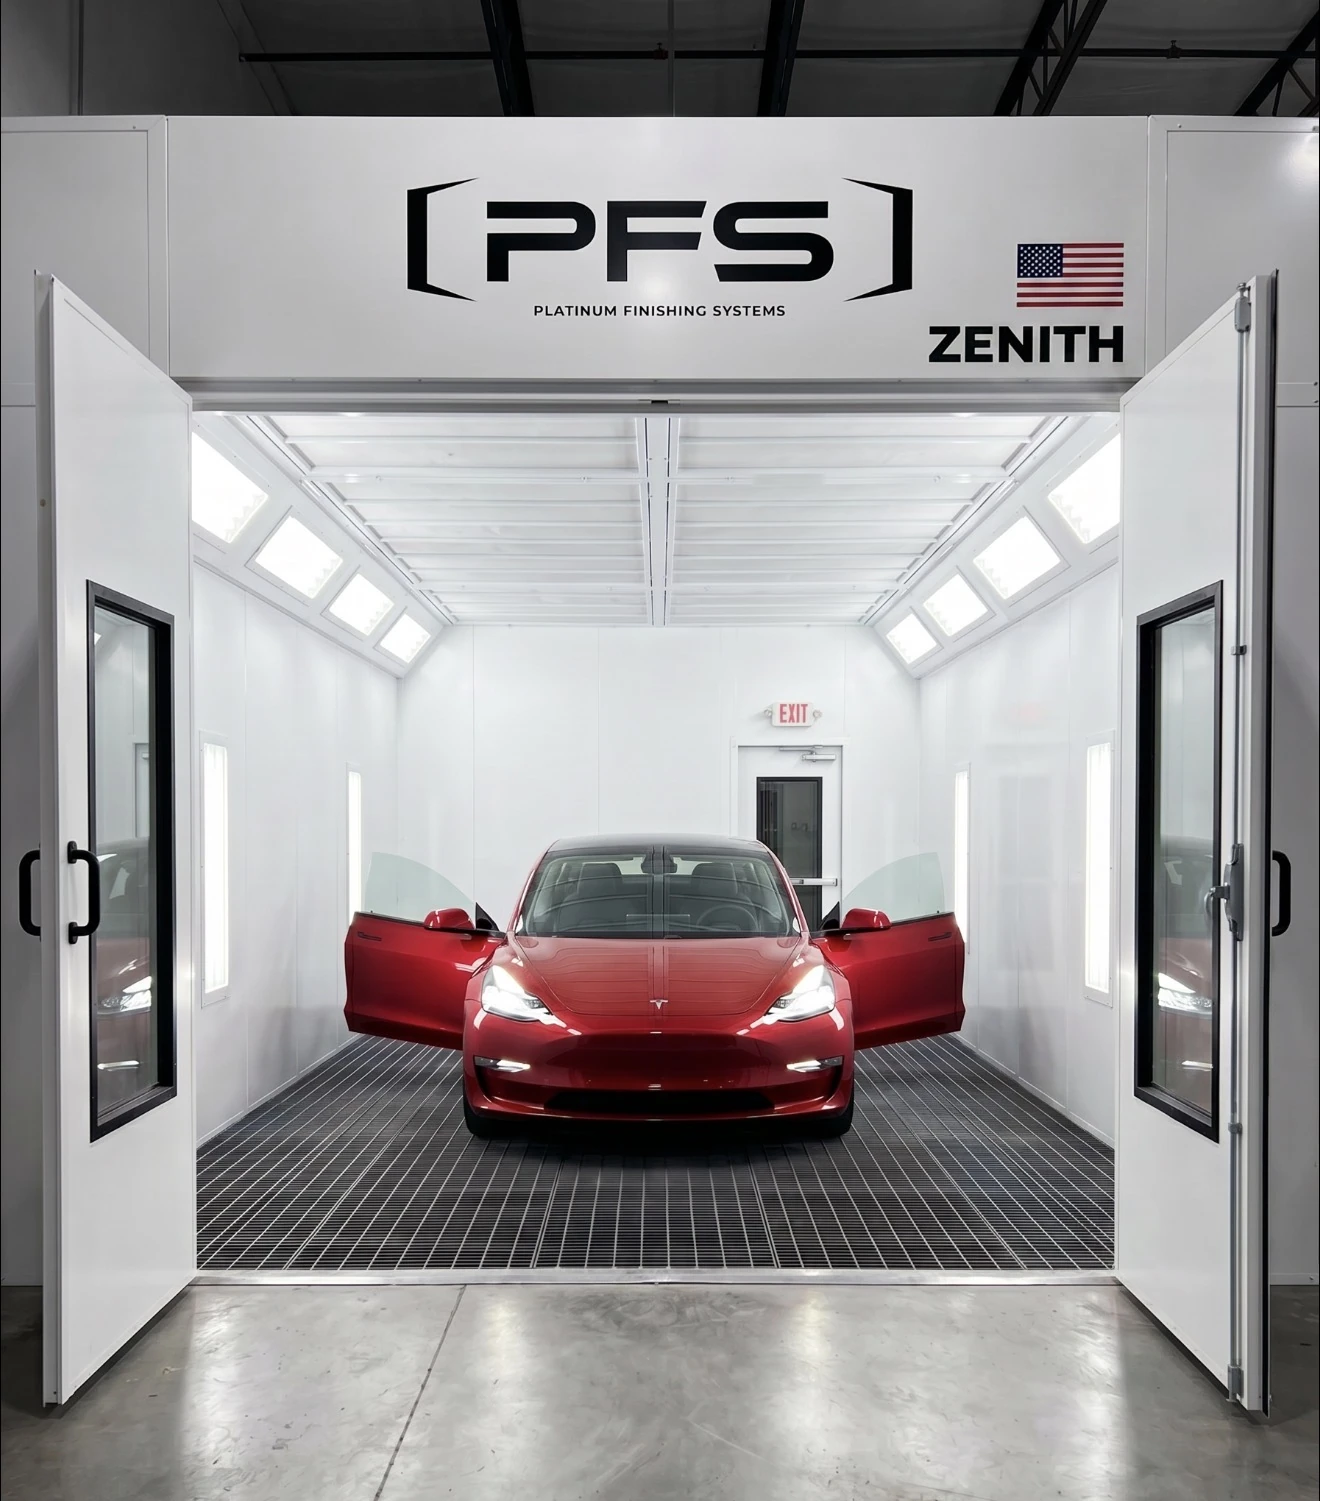
Full-enclosure booths for superior overspray containment and finish quality.

Robotic finishing cells for precise, repeatable automated spray application.
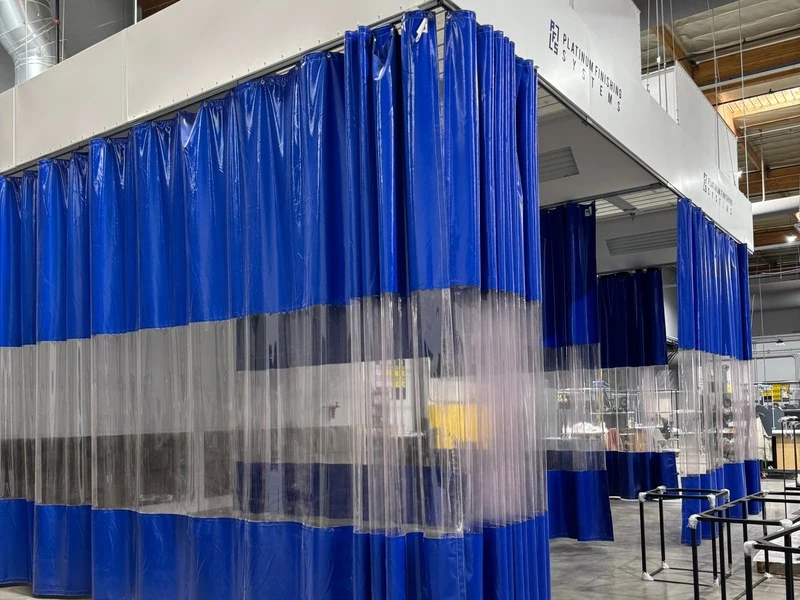
Dedicated prep and masking stations to keep your spray booth running at full capacity.

Complete powder coating lines: pretreatment, booth, powder recovery, cure oven, and conveyor.
Automotive paint booths for production: Platinum Finishing Systems (PFS) builds full downdraft, semi-downdraft and side downdraft automotive spray booths, robotic finishing cells and integrated finishing lines with cure ovens and air make-up, ETL listed, built to NFPA 33 and made in the USA.