Continuous conveyor ovens for high-volume powder curing and paint baking on automated finishing lines.


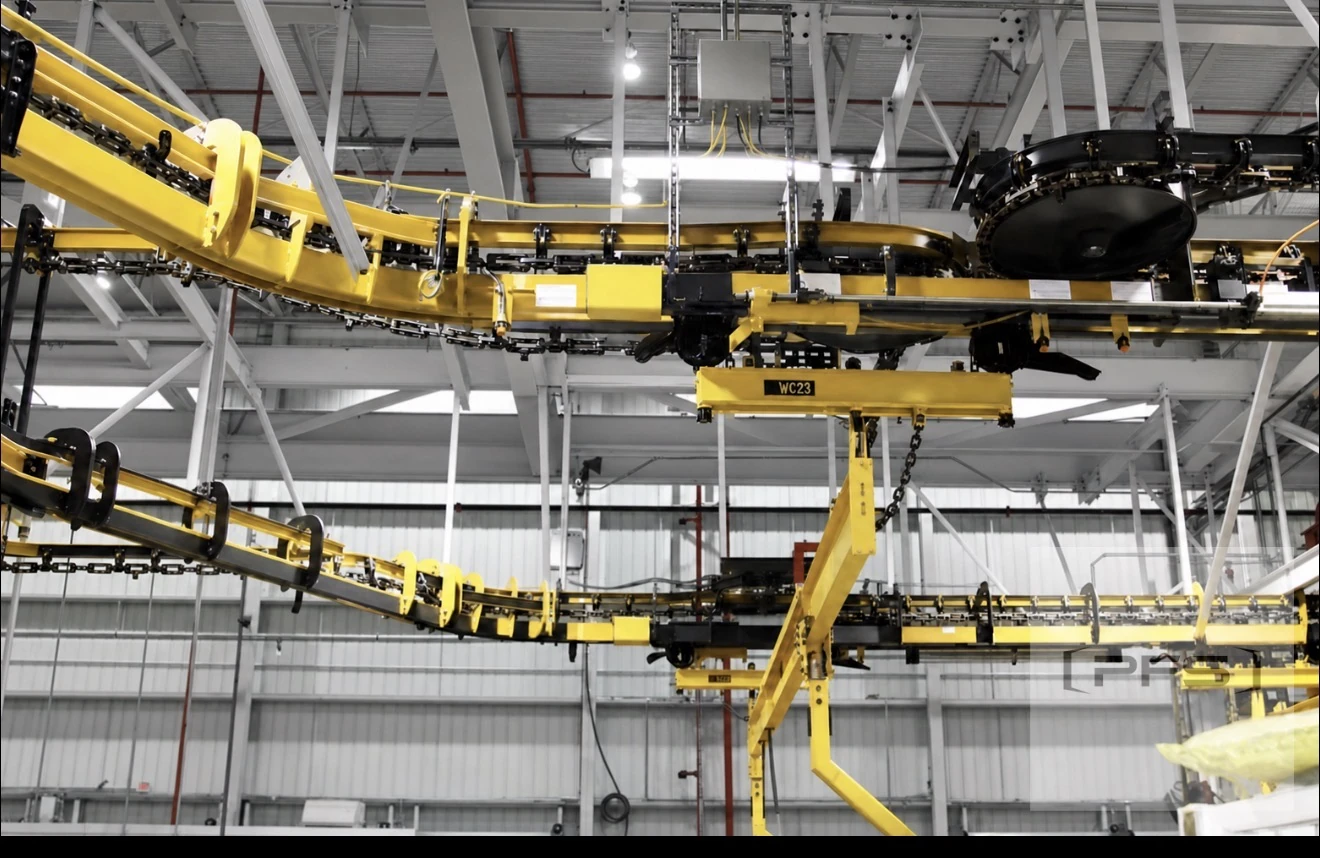
PFS conveyor ovens integrate with overhead and floor conveyor systems for continuous, high-volume curing. Designed for production environments where throughput and consistency are critical.
Our engineers are available to help you select the right configuration for your application.
Parts must stay at cure temperature for the full cure time while moving. The faster the line, the longer the oven. That is why line speed, part load and coating chemistry are the first numbers PFS asks for.
The oven opening is sized around the largest part on the conveyor with clearance, kept as small as practical to hold heat in.
Conveyor ovens work with overhead and floor conveyor systems. The conveyor path through the oven, including any passes or turns, is laid out with the rest of the line.
Gas is common on high-volume lines. Electric suits smaller ovens and sites without gas service.
A typical powder line runs pretreatment systems, a dry-off oven, the powder booth and the cure oven, all on one conveyor. See conveyor systems and the full powder coating line.
An infrared booster zone ahead of the convection oven can bring parts up to temperature faster.
Send your line speed, part sizes and cure schedule. We will size and quote it.
A continuous curing oven that parts pass through on an overhead or floor conveyor, used for high-volume powder curing and paint baking.
By line speed, part size and the cure schedule of your coating. Those set the oven length, opening size and heat input.
Both are available. Gas is common for high-volume lines; electric suits smaller ovens and places without gas service.
Yes. Ovens can be laid out with washers, dry-off ovens, powder booths and conveyors as one system.
PFS conveyor ovens are ETL/UL certified and built to NFPA 86.
Yes. Conveyor ovens are used for powder curing and paint baking on automated finishing lines.
Yes. Lengths and widths are matched to your line speed, part size and cure schedule.
Long enough to bring the metal to the temperature in your coating maker’s cure schedule and hold it there for the full cure time. Dwell time is the oven conveyor length divided by line speed. Heavy parts take longer to heat than thin sheet metal, so part mass matters as much as line speed.
Parts must stay at cure temperature for the full cure time while they move, so the faster the line, the longer the oven. An infrared booster zone ahead of the convection oven can bring parts up to temperature faster. Line speed, part load and coating chemistry are the first numbers we ask for.
A typical line runs pretreatment, a dry-off oven, the powder booth and the cure oven, all on one conveyor. See powder coating lines and conveyor systems.
Overhead monorail, power-and-free, and floor conveyor systems for industrial finishing lines.
Complete powder coating lines: pretreatment, booth, powder recovery, cure oven, and conveyor.
Automated chemical pretreatment systems for cleaning, phosphating, and surface prep before coating.